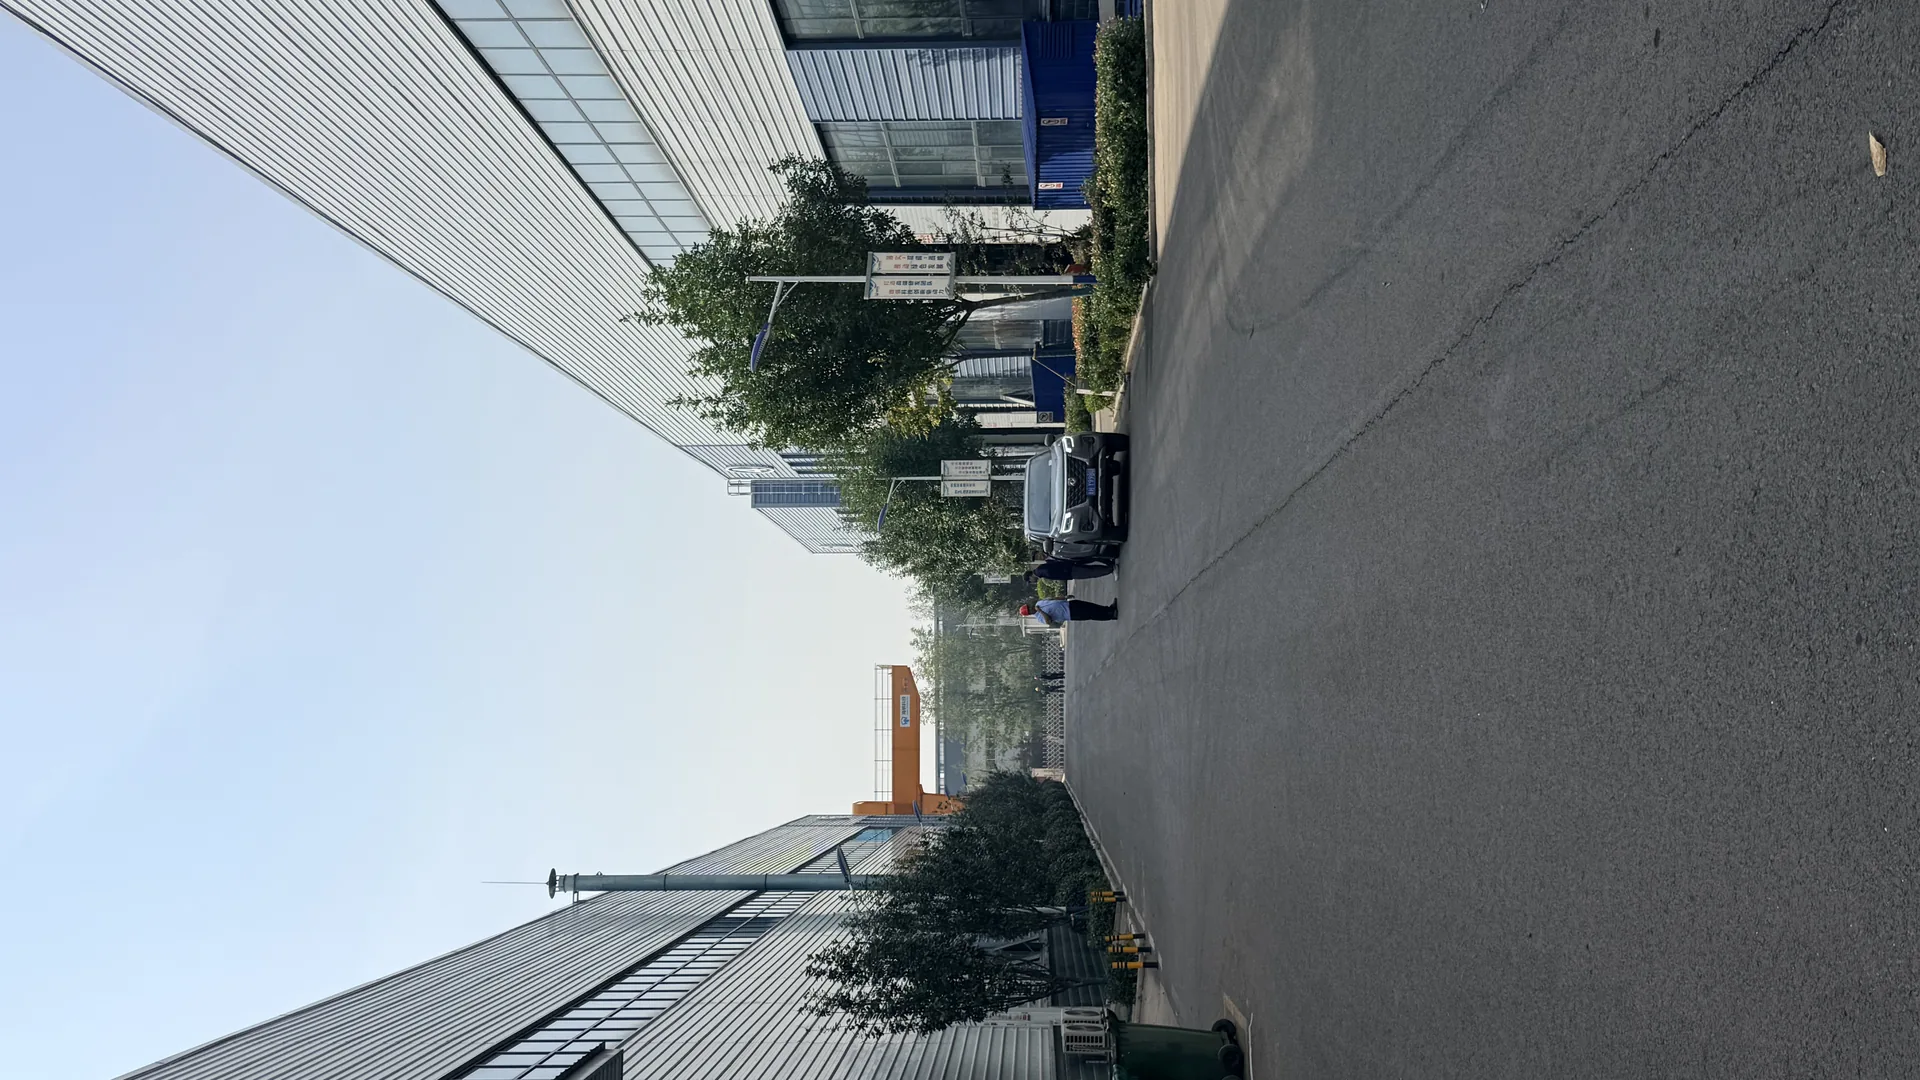
Our factory
We machine, assemble and test hydraulic valves for powered roof supports in our own workshops. This page describes what is actually there, so that a buyer or a distributor can judge us before travelling.
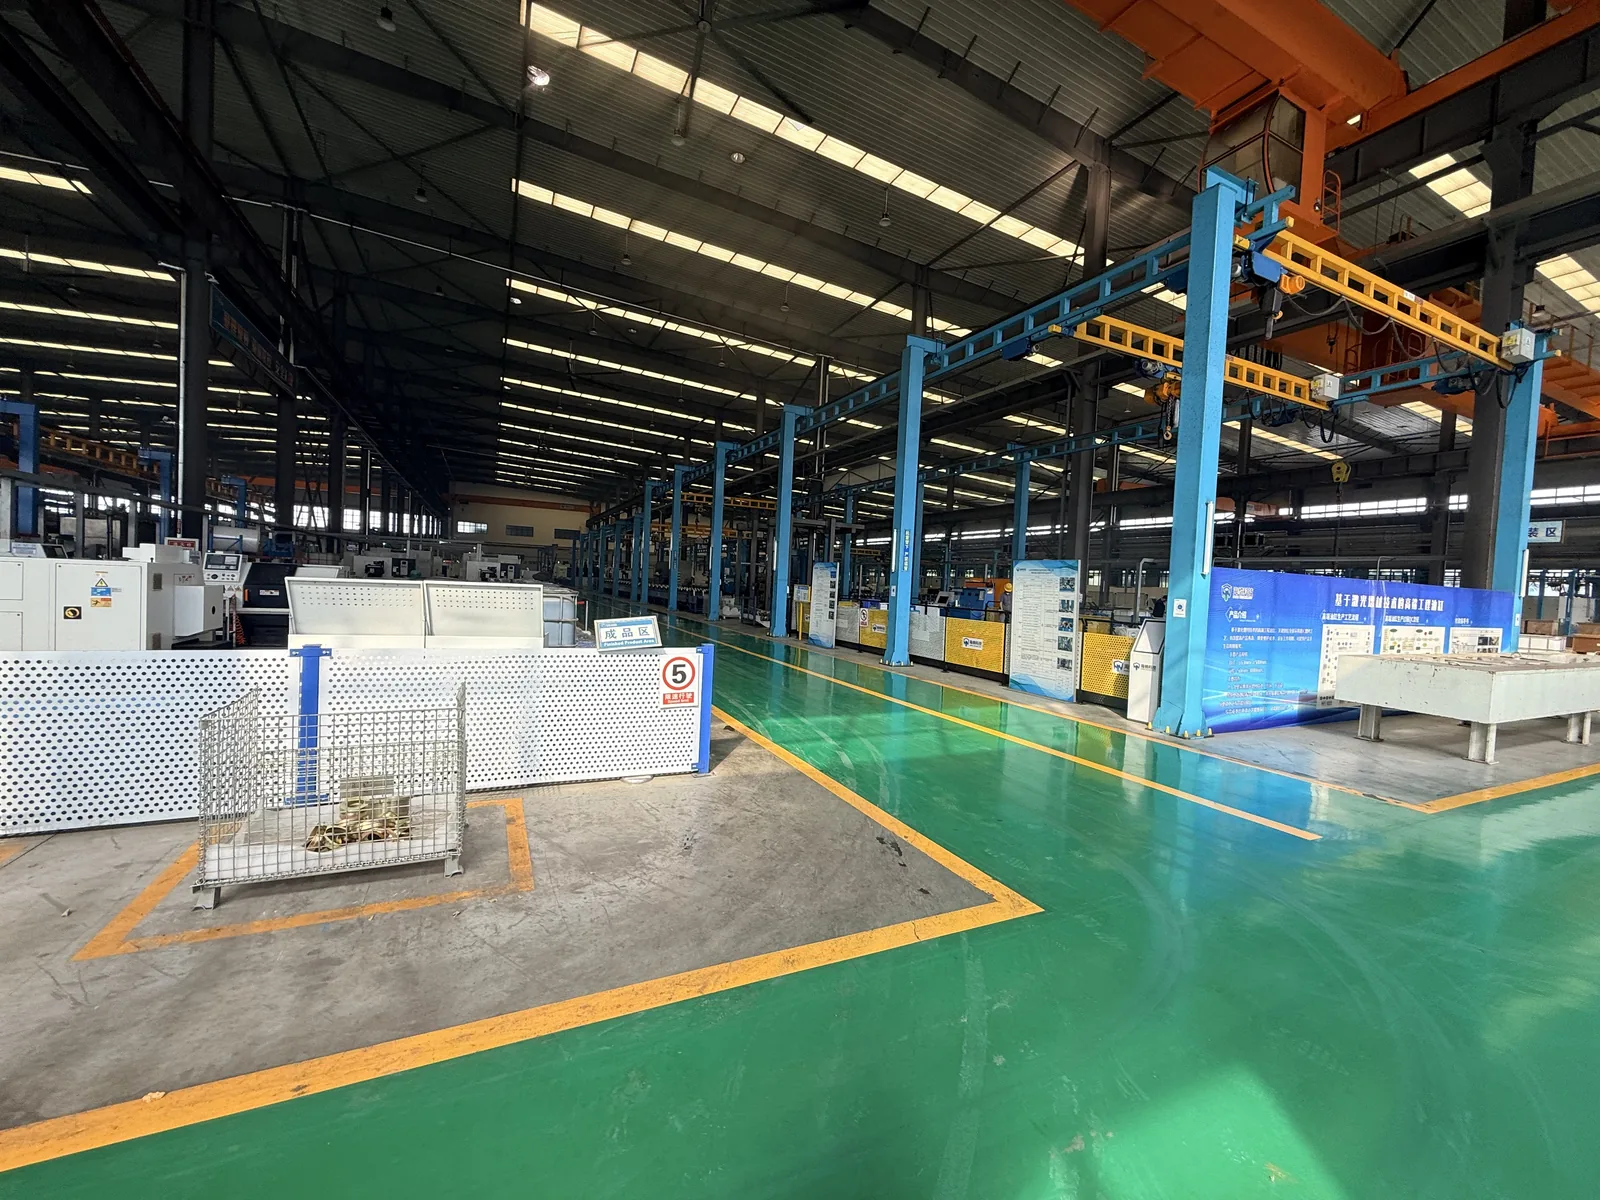
Machining, assembly and testing under one roof
Valve blocks are machined on horizontal machining centres, cleaned, assembled and pressure-tested in the same plant. Keeping these steps together is what makes a one-off replacement part practical: when a dimension does not come out as expected, the machinist, the fitter and the inspector are in the same building rather than in three different companies.
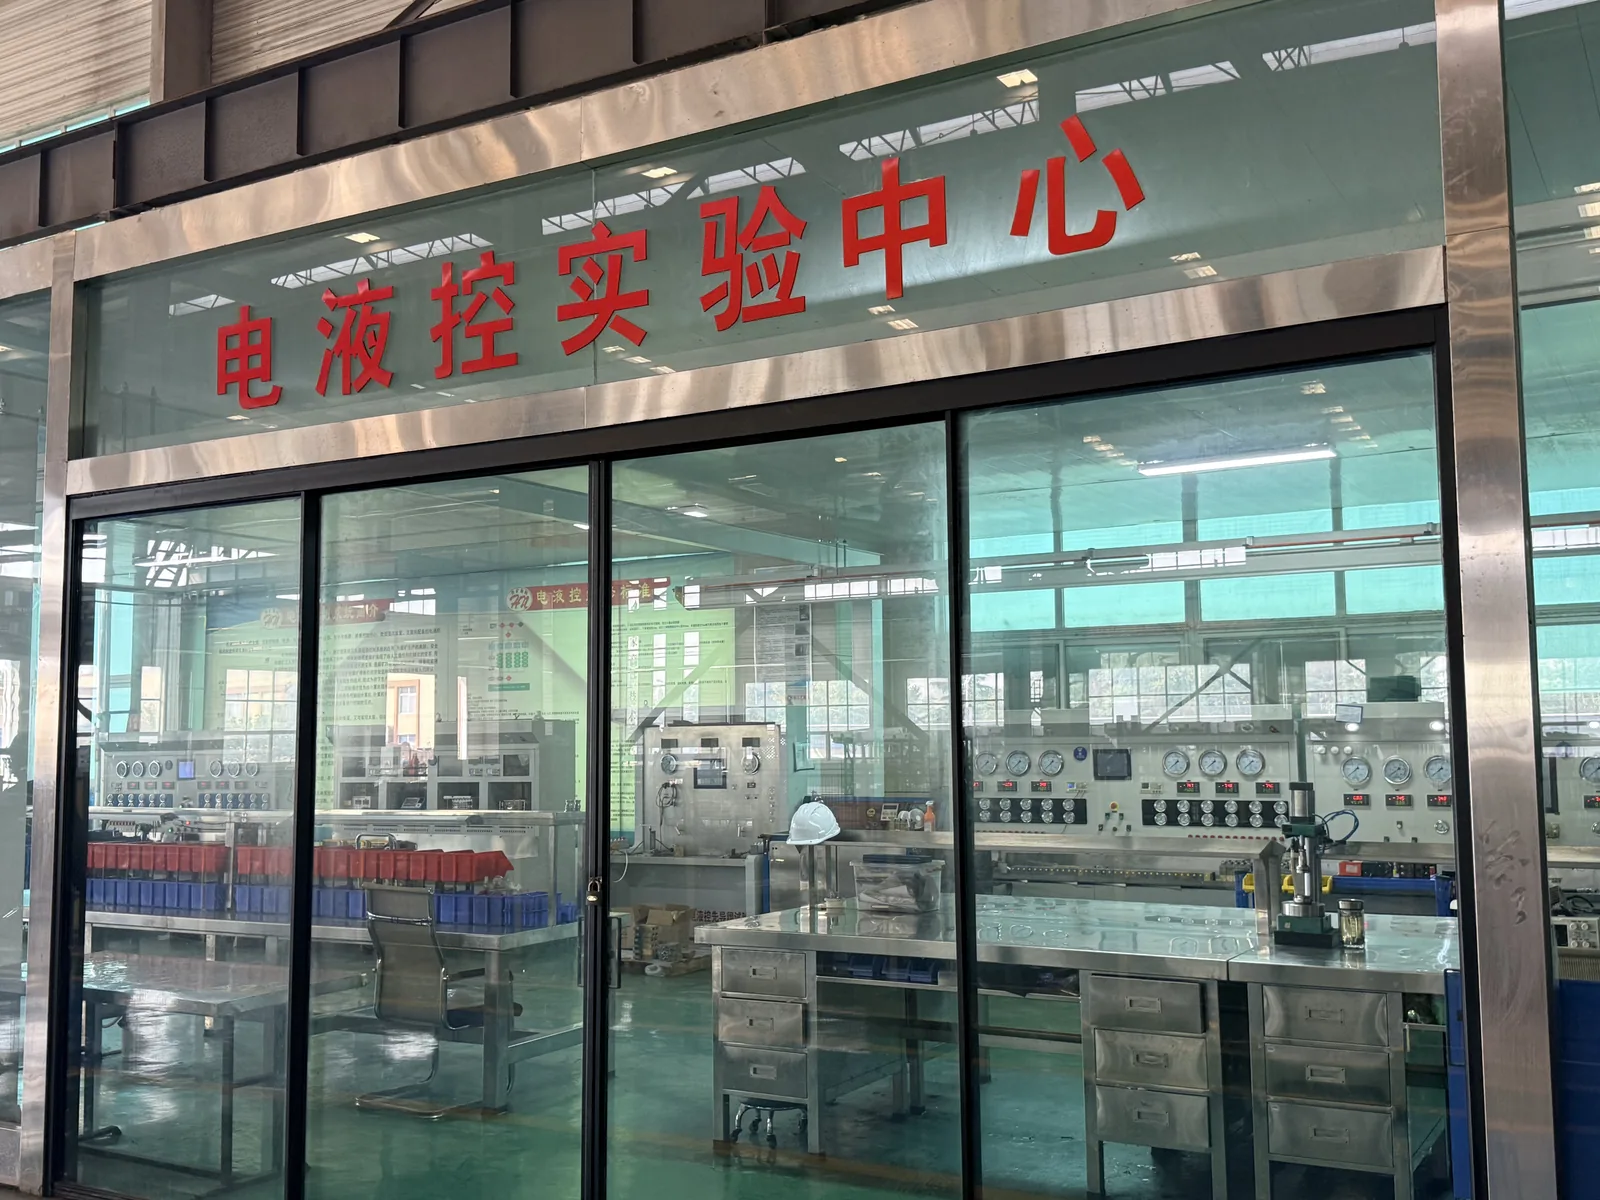
Electro-hydraulic control laboratory
Electro-hydraulic valve banks and support controllers are a different discipline from plain hydraulics, so they are developed and tested in a separate laboratory with its own test benches. This is where a new control configuration is proven before it goes anywhere near a mine.
Pressure testing before dispatch
Assembled valves are pressure tested before packing, and the test bench record is kept against the batch. Test records can be supplied with the shipment on request. What we will not do is describe a test we did not run — if a certificate is required, say so at the quotation stage and it will be produced from the actual test.
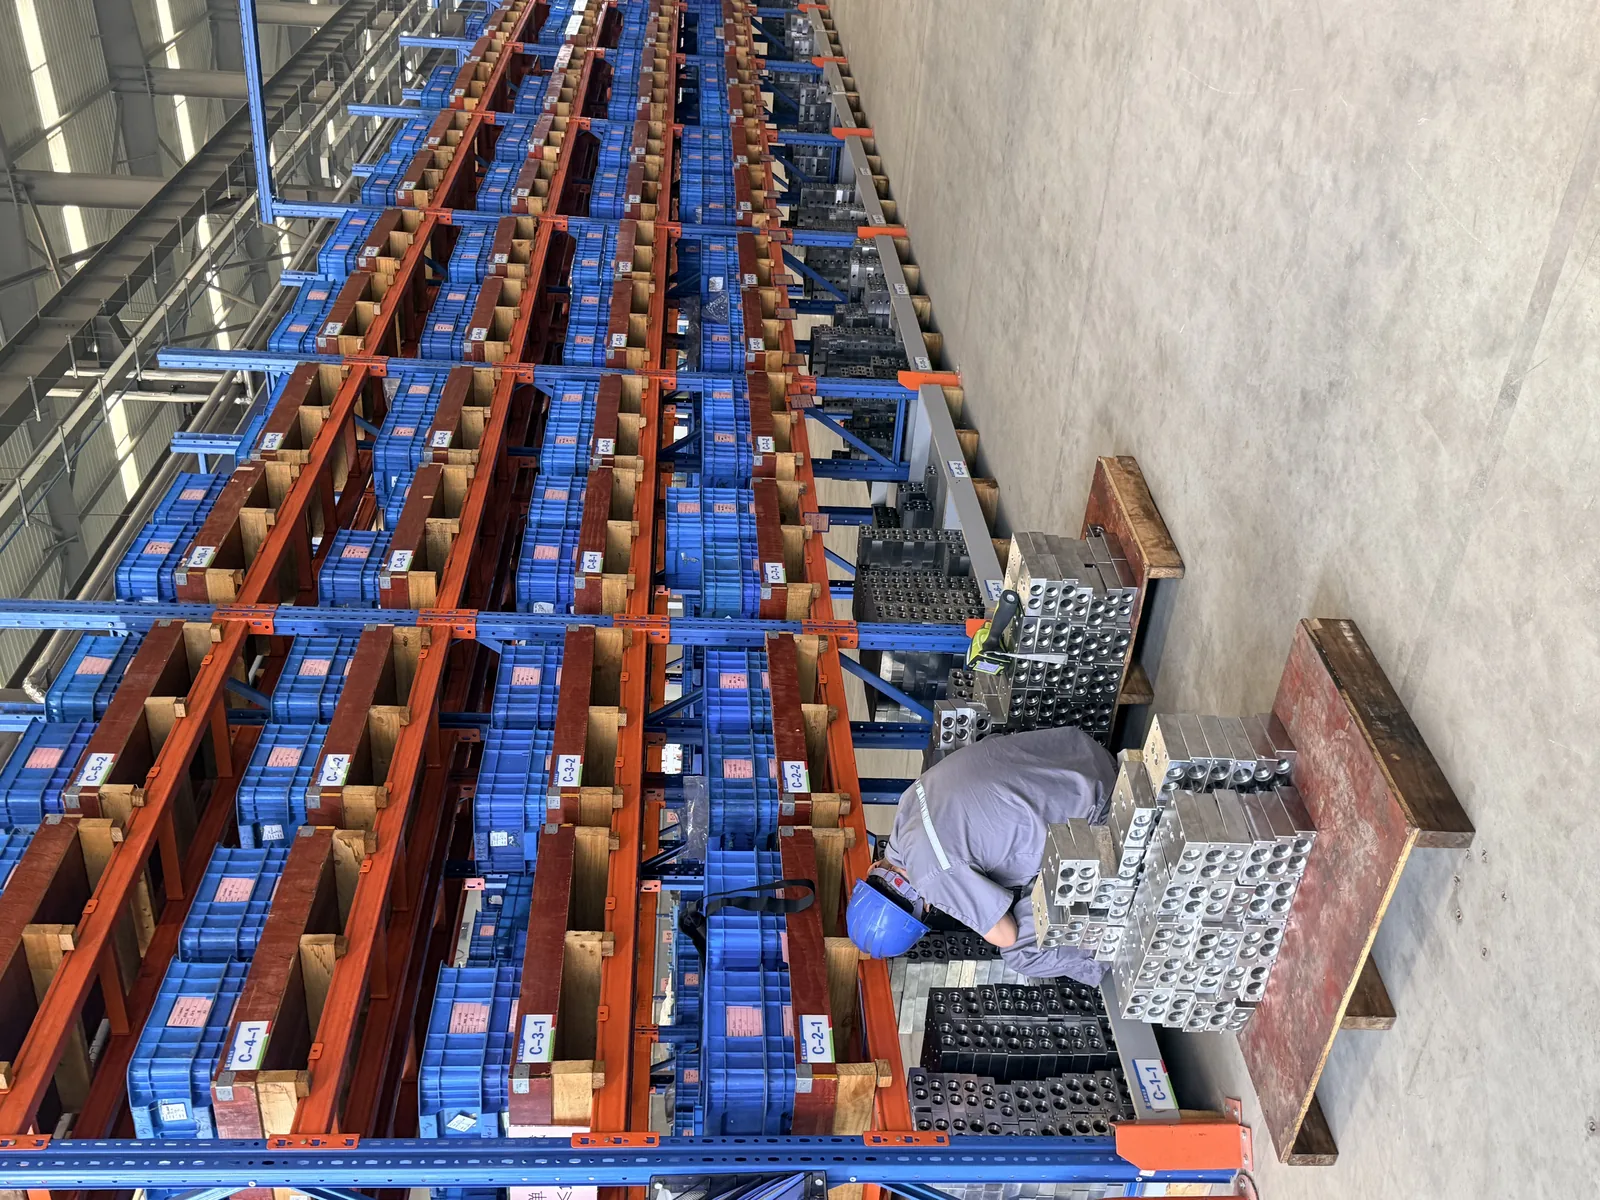
Stock and delivery
Finished parts are held in a racked store with location numbering, which is how we can pull a repeat order quickly rather than remanufacture it. For a distributor this matters more than the price list: the part the customer needs is either on the shelf or it is a month away.
Come and see it
Distributors and larger buyers are welcome to visit, and we would rather you did before committing to stock. Tell us which part families you intend to carry and we will have the relevant lines and the test records ready. Arrange a visit.